Solution topic
Non-standard container sealing prototyping: validate with representative samples first, then design changeover tooling
For irregular cups, trays, and non-standard bottles, pails, and cans, first complete bench-top trial sealing with container and film samples, then design tooling and production rou
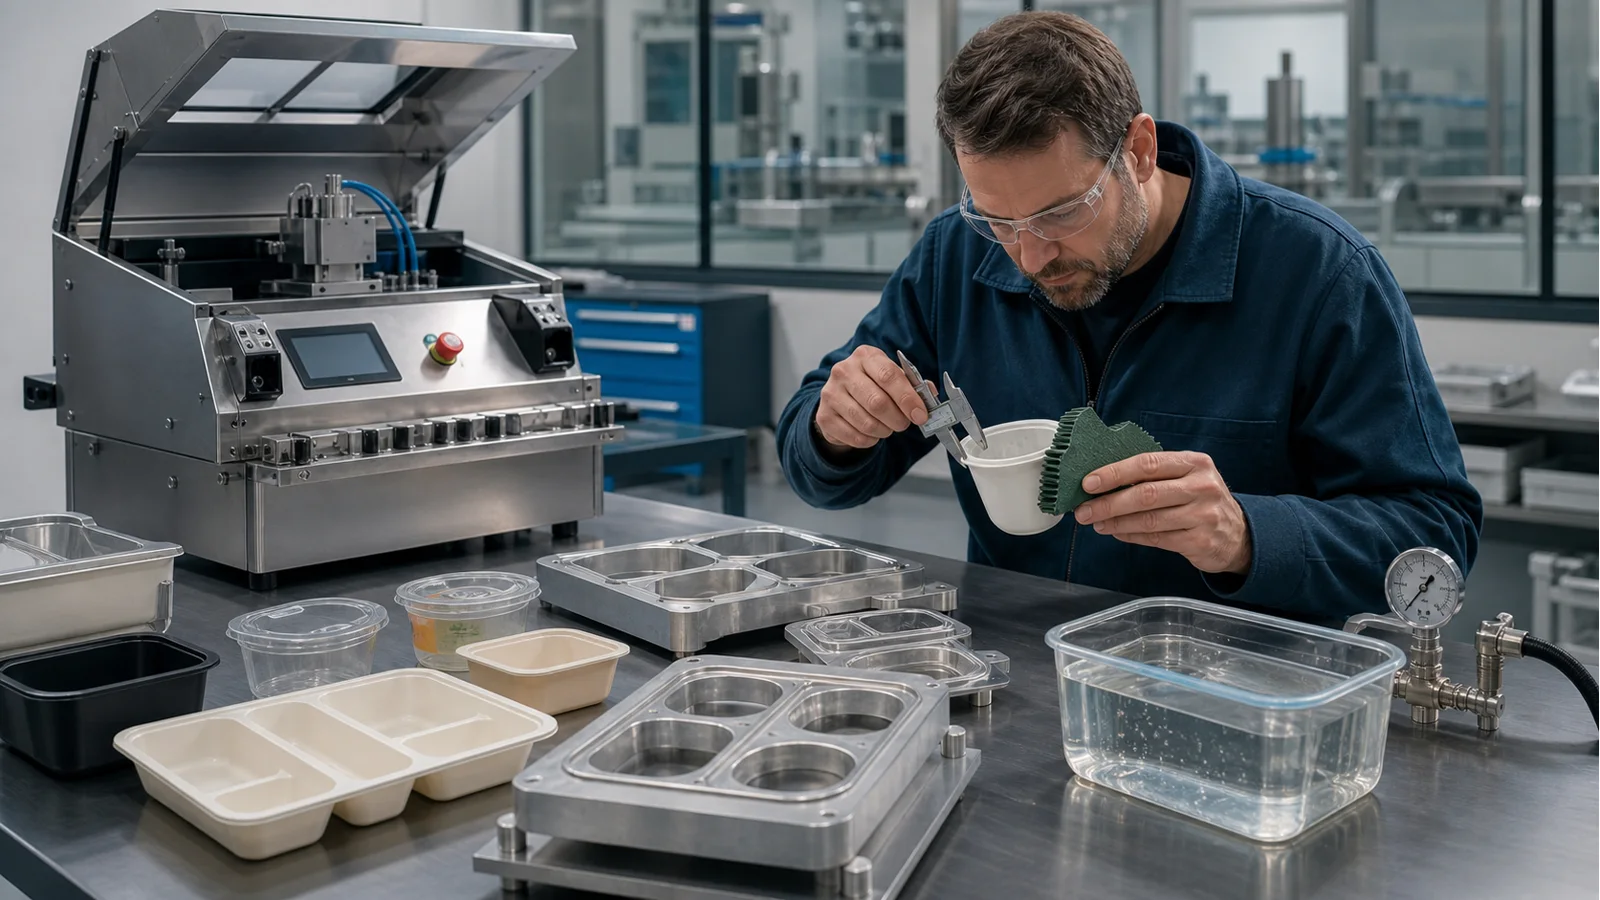
- Irregular cups, trays, and bottle, pail, and can containers should first verify rim, film material, and sealing contact surface; bench-top trial results cannot be directly equated to production line integration. Provide representative containers and film samples, rim drawings, test purpose, changeover checklist, target capacity, and downstream requirements.
Solution summary prepared for you
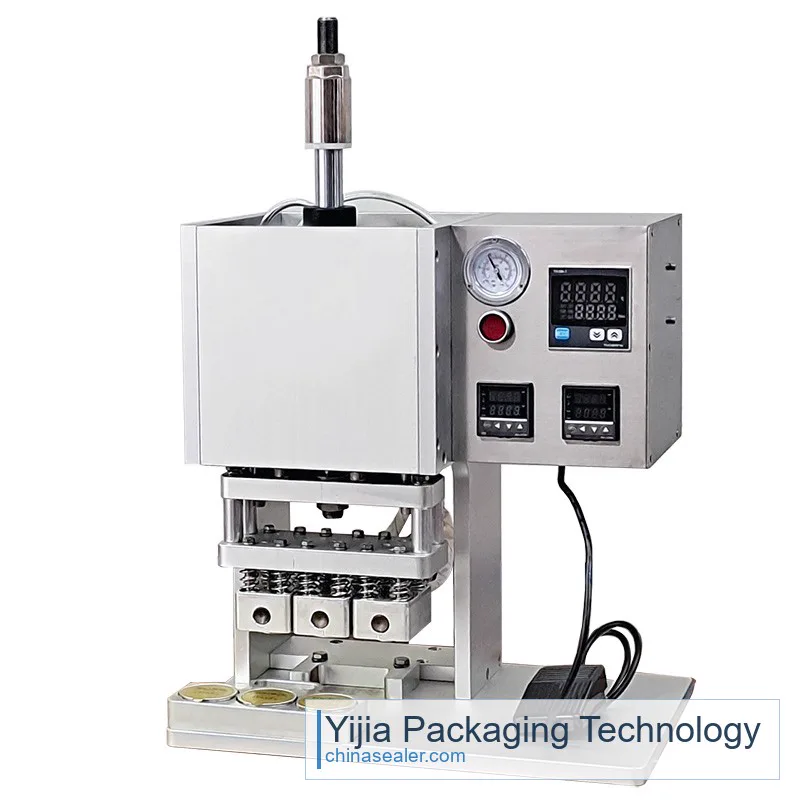
- For non-standard container sealing, first verify the contact surface with representative containers and films. Small-diameter can use SGP-03, and tray roll film can use a bench roll-film tray sealing machine.
- Bench sealing tests only confirm the single-sample process; after representative samples and fixtures are stable, evaluate the multi-station and changeover of the rotary vacuum tray sealing machine.
- Special bottle mouths and drum mouths use an in-line bottle heat sealing machine or a large-diameter drum heat sealing machine respectively, and the mass production downstream section verifies automatic conveying and checkweighing/vision.
Route comparison
- Suitable for the stage when the non-standard container process is not yet confirmed and the rim, film, heat sealing contact, and basic positioning need to be verified first.
- Small-diameter and trays use corresponding bench equipment, which can quickly distinguish cup film sealing and roll film cutting issues.
- Bench results only cover representative samples and single-station actions; they cannot explain automatic feeding, multi-station, continuous cycle time, or mass production inspection.
- When representative samples, films, and test purposes are not yet clear, do not make complete mass production fixtures or lines first.
- Small-diameter containers use the small-diameter cup sealing machine SGP-03, and trays use the bench roll-film tray sealing machine.
- Suitable for tray projects where the representative sample sealing process is stable and further verification of multi-station positioning, vacuum tasks, and specification changeover is needed.
- The rotary vacuum tray sealing machine allows fixtures, stations, and changeover records to enter continuous cycle verification.
- Positioning fixtures, bottom support, pressure head, vacuum tasks, and reset methods all need to be determined based on physical samples; a single seal appearance is not enough to finalize.
- When the rim film is still being screened, or the container specifications have not formed a representative sample list, keep the bench sealing test first.
- Multi-station verification uses the rotary vacuum tray sealing machine with changeover fixtures formed from physical samples.
- Suitable for containers with special bottle mouths or drum mouths, or when the main sealing and fixtures are stable and conveying and inspection need to be verified.
- Bottle and drum main machines are separated by rim, while automatic conveying and checkweighing/vision are verified at the mass production stage to avoid confusing sample and production conclusions.
- The rim film, fixtures, cycle time, defective product samples, and site layout all need to be confirmed; the downstream section cannot be inferred directly from bench data.
- When the project is still screening containers or films, or the changeover boundaries are not yet clear, do not enter the mass production downstream line.
- Bottle mouths use the in-line bottle heat sealing machine, drum mouths use the large-diameter drum heat sealing machine, and the downstream section uses the automatic conveying line and online checkweighing/vision system.
Associated Equipment / Consumables
 Benchtop Roll-Film Tray Sealing Machine
A benchtop roll-film sealer for manually loaded cups, bowls and trays. Trial the rim and ribs, lidding seal layer, tooling fit, trimming, peel and leak result as one system. Compare MAP or continuous filling-sealing e...
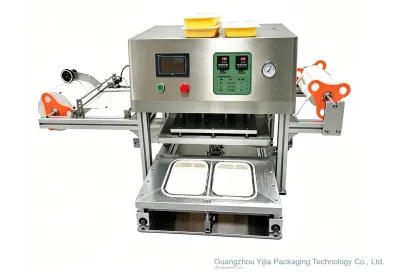 Tabletop Multi-Compartment Meal Tray Sealer
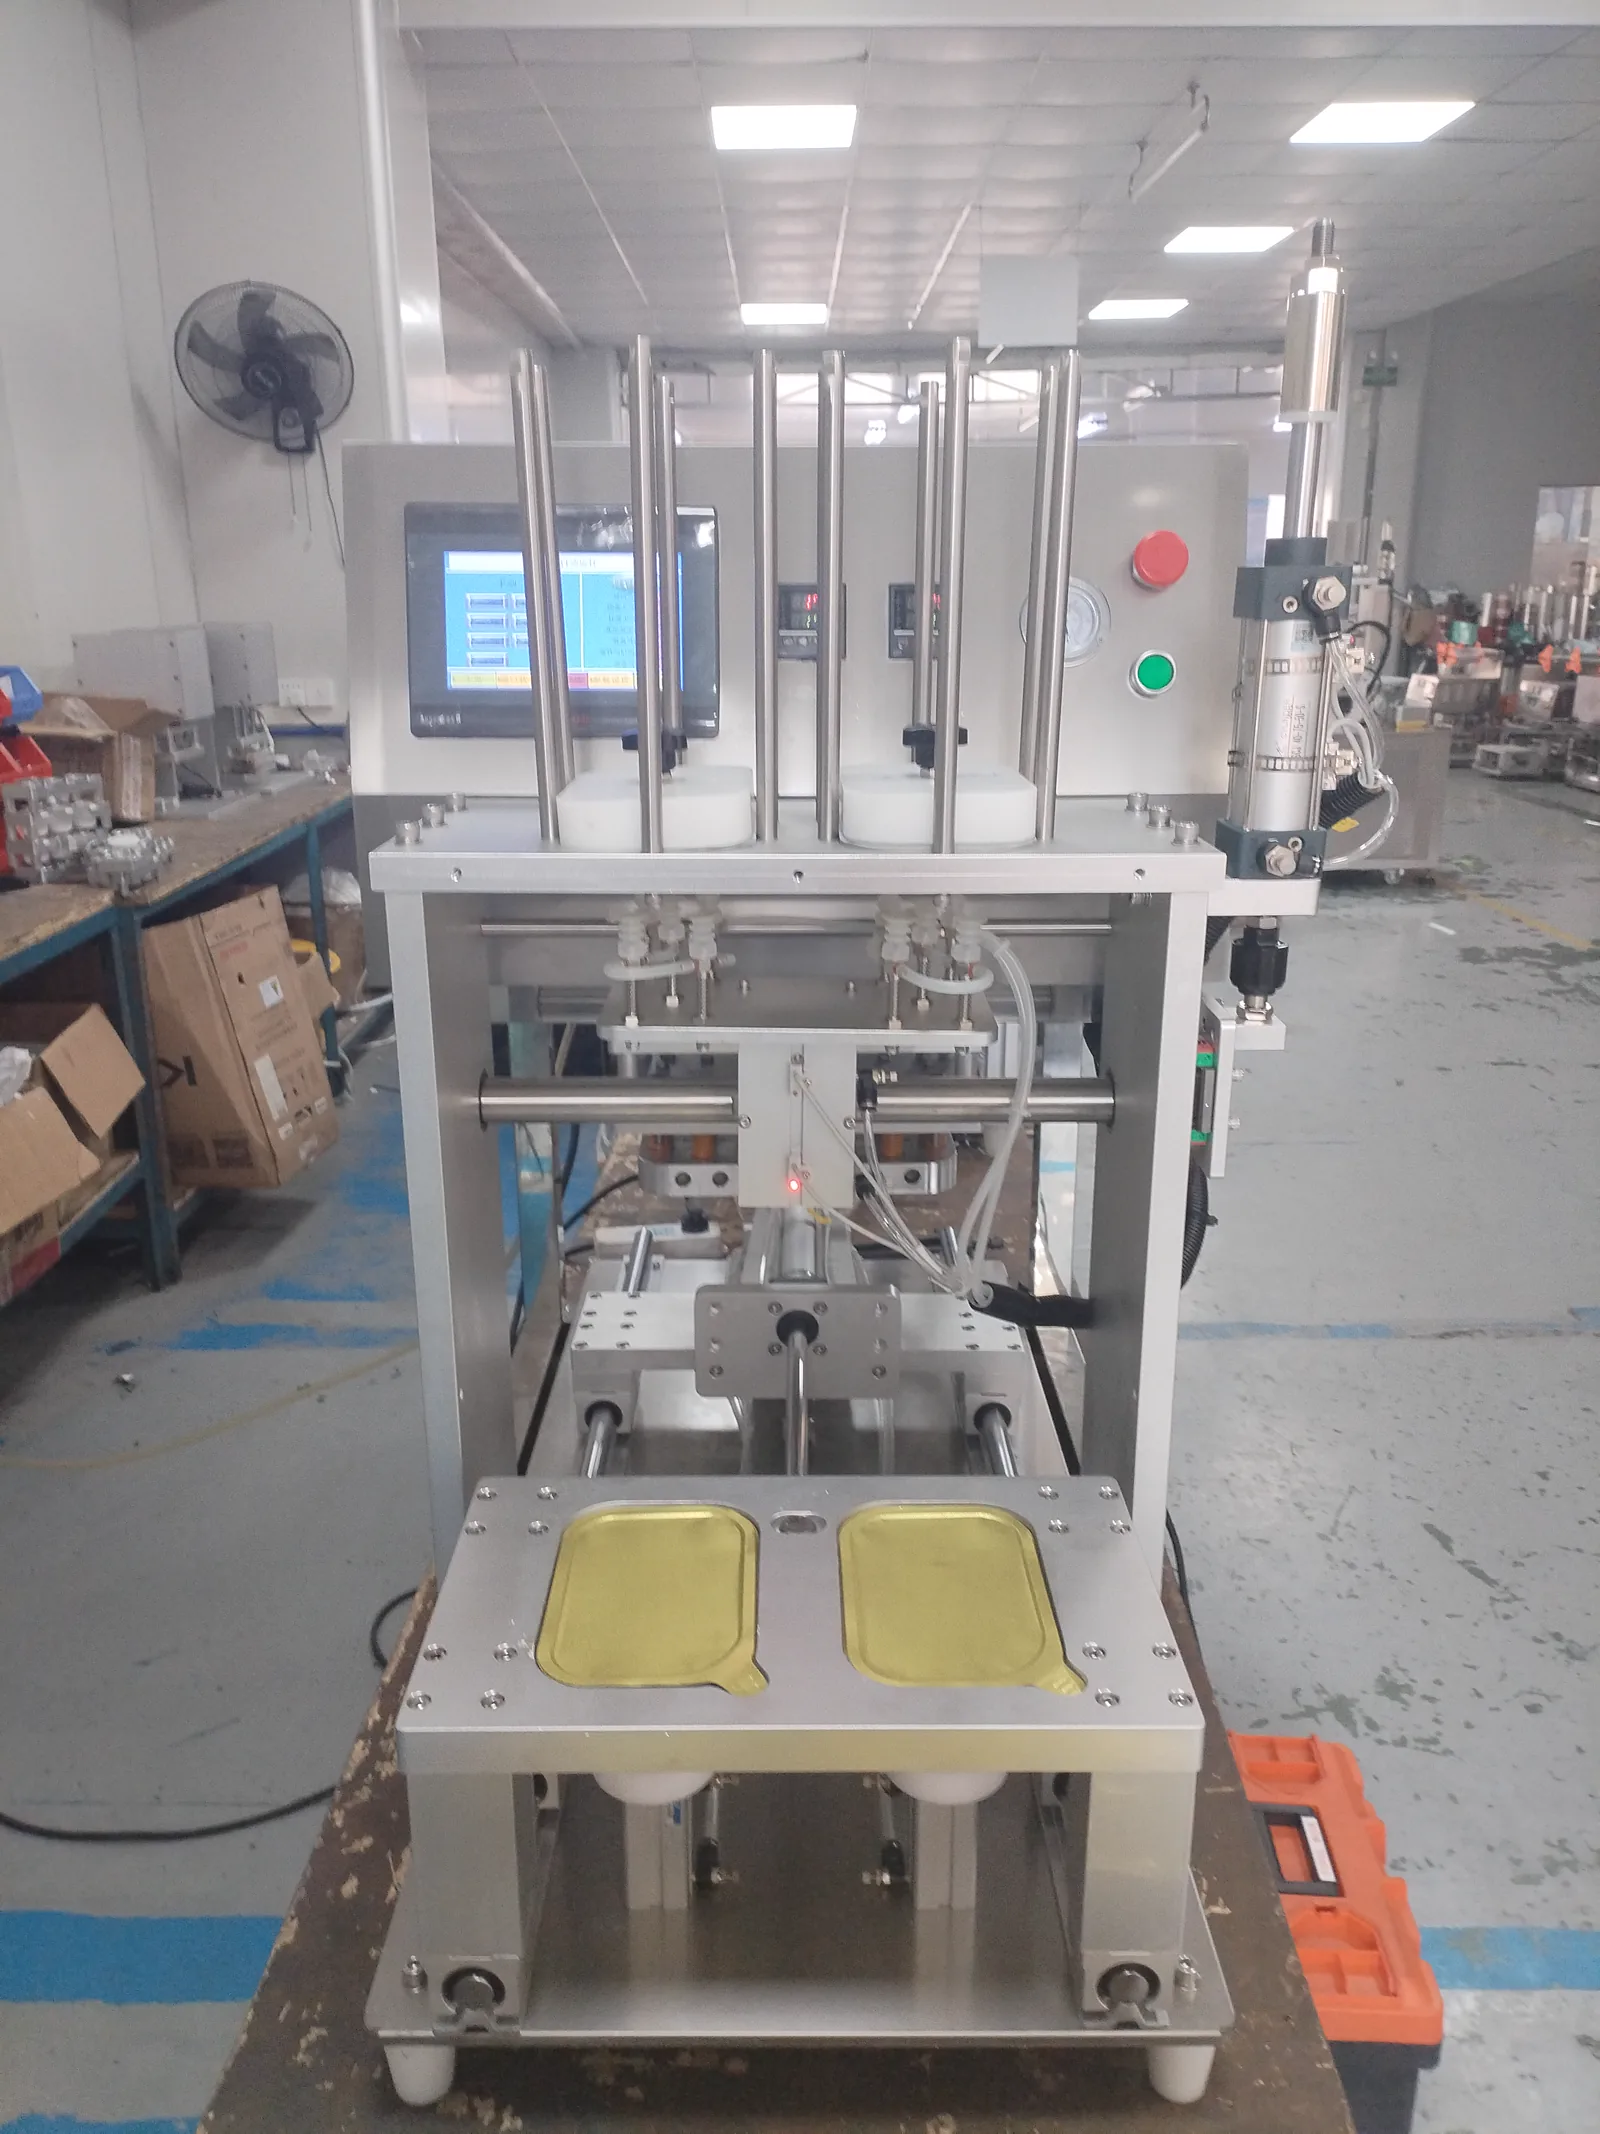 Automatic Pre-Cut Lid Pick-and-Place Tray Sealer
 Small-Diameter Cup Sealer SGP-03
Core process
Sample details
Representative samples are used to determine the sealing test equipment, bottom support, pressure head, and fixture positioning; photos only help with initial branching.
Provide container samples covering the main materials, rims, deformations, and specification differencesSeal the film and rim as a pair, and record the contact surface, film positioning, roll film cutting, and opening status.
Submit roll film, pre-cut film, or easy-tear film, and indicate the corresponding containerDimension drawings are used to explain intent, while physical samples are used to observe local deformation and support; both support fixture design.
Provide the mouth diameter, rim width, height, sealing area, and allowable compression positionsOnly after clarifying the test purpose can you choose between bench sealing, rotary vacuum tray equipment, or special bottle/drum heat sealing branches.
List the heat sealing, vacuum, opening, appearance, or other items to be verified and the acceptance criteriaThis information is used to verify fixture disassembly and reset, multi-station operation, and mass production automatic conveying conditions.
List the specification list, changeover frequency, planned cycle time, and upstream feeding methodAfter the main sealing process is stable, arrange the automatic conveying line and online checkweighing/vision system accordingly.
Explain finished product conveying, weight recheck, visual inspection, defective product handling, and available floor spaceCommon selection mistakes
View detailed technical notes
Non-standard sealing starts with representative samples, not equipment names
Irregular cups, non-standard trays, and special bottles, pails, and cans differ in rim, material, and compression state; first establish a corresponding list of representative samples and film materials.
Test purpose determines the trial sealing equipment
Heat sealing of small-diameter cup film, roll-film cutting and sealing for trays, vacuum tasks, and direct heat pressing for bottles and pails are different validations and cannot be covered by one general-purpose machine.
Use SGP-03 to understand heat sealing for small-diameter containers first
The small-diameter cup sealing machine SGP-03 is used for initial trial sealing of the rim and film material of representative samples; the results do not include production feeding and inspection and serve only as a basis for process screening.
Use bench-top equipment to validate roll-film trays
The bench-top roll-film tray sealing machine is used to observe roll-film feeding, film cutting, tray positioning, and rim sealing; the tooling is adjusted step by step based on actual samples and retained for reference.
Tooling design focuses on support and repeatable positioning
The positioning fixture, bottom support, and pressing head must not only accommodate the container but also maintain sealing contact and specified appearance after repeated clamping; each specification requires checking the reset state.
Multi-station validation comes after single-station process confirmation
After the representative samples and tooling are stable, use the rotary vacuum tray sealing machine to validate multi-station operation, vacuum tasks, and changeover reset.
Bottle mouths and pail mouths enter dedicated branches separately
For special bottle mouths, evaluate the inline bottle heat sealing machine; for large-diameter pail mouths, evaluate the pail heat sealing equipment; each uses the corresponding rim and film material.
Production line integration is not a scale-up of bench-top results
Automatic conveying changes container orientation, and checkweighing and vision inspection also require defective-product handling and judgment methods; the downstream section must be separately validated under production conditions.
The changeover checklist runs from sample to production
Each specification should record tooling, parameters, reset, and first-article inspection steps; the production plan is evaluated accordingly for changeover and cycle time.
Common questions
Can a preliminary sealing test be determined from photos of non-standard containers only?
Start by identifying the container type, rim, and film format to make an initial distinction between small-diameter, roll-film tray, or bottle/drum branches. The fixture design still needs to be based on representative samples.
How should representative samples be selected?
It should cover the main differences in rim, material, rigidity, deformation, and specifications, and be paired with the corresponding film and finished seal targets.
Can a production line be designed directly after bench sealing tests pass?
No. Bench results only indicate the heat sealing relationship for a specific sample; mass production still requires verification of feeding, positioning, fixture reset, cycle time, and handling of defective products.
When should a rotary vacuum tray sealing machine be evaluated?
When the representative sample process and fixture positioning are stable, and further verification of multi-station and changeover is needed, then proceed to rotary table equipment trials.
Do all irregular bottles, drums, and cans use the same heat sealing machine?
No. Bottle mouths and large-diameter drum mouths should be evaluated separately with bottle or drum heat sealing equipment based on their respective dimensions, support methods, and films.
What prerequisites are needed for the post-production section?
After the container samples, fixtures, process parameters, changeover list, and cycle time are stable, then verify the automatic conveying line and online checkweighing/vision system.