Check applicable objects first
Pre-made bags with uniform specifications, consistent bag mouth, and continuous bag supply; special zipper bags or irregular bags require separate trials
Four-lane parallel pouch packaging
Coordinates premade-pouch feeding, opening, dosing, filling, heat sealing and discharge across four lanes. Use actual pouches and product to confirm opening stability, dosing time, clean pouch mouths, seal dwell and merged discharge; four lanes alone do not establish a fixed output.
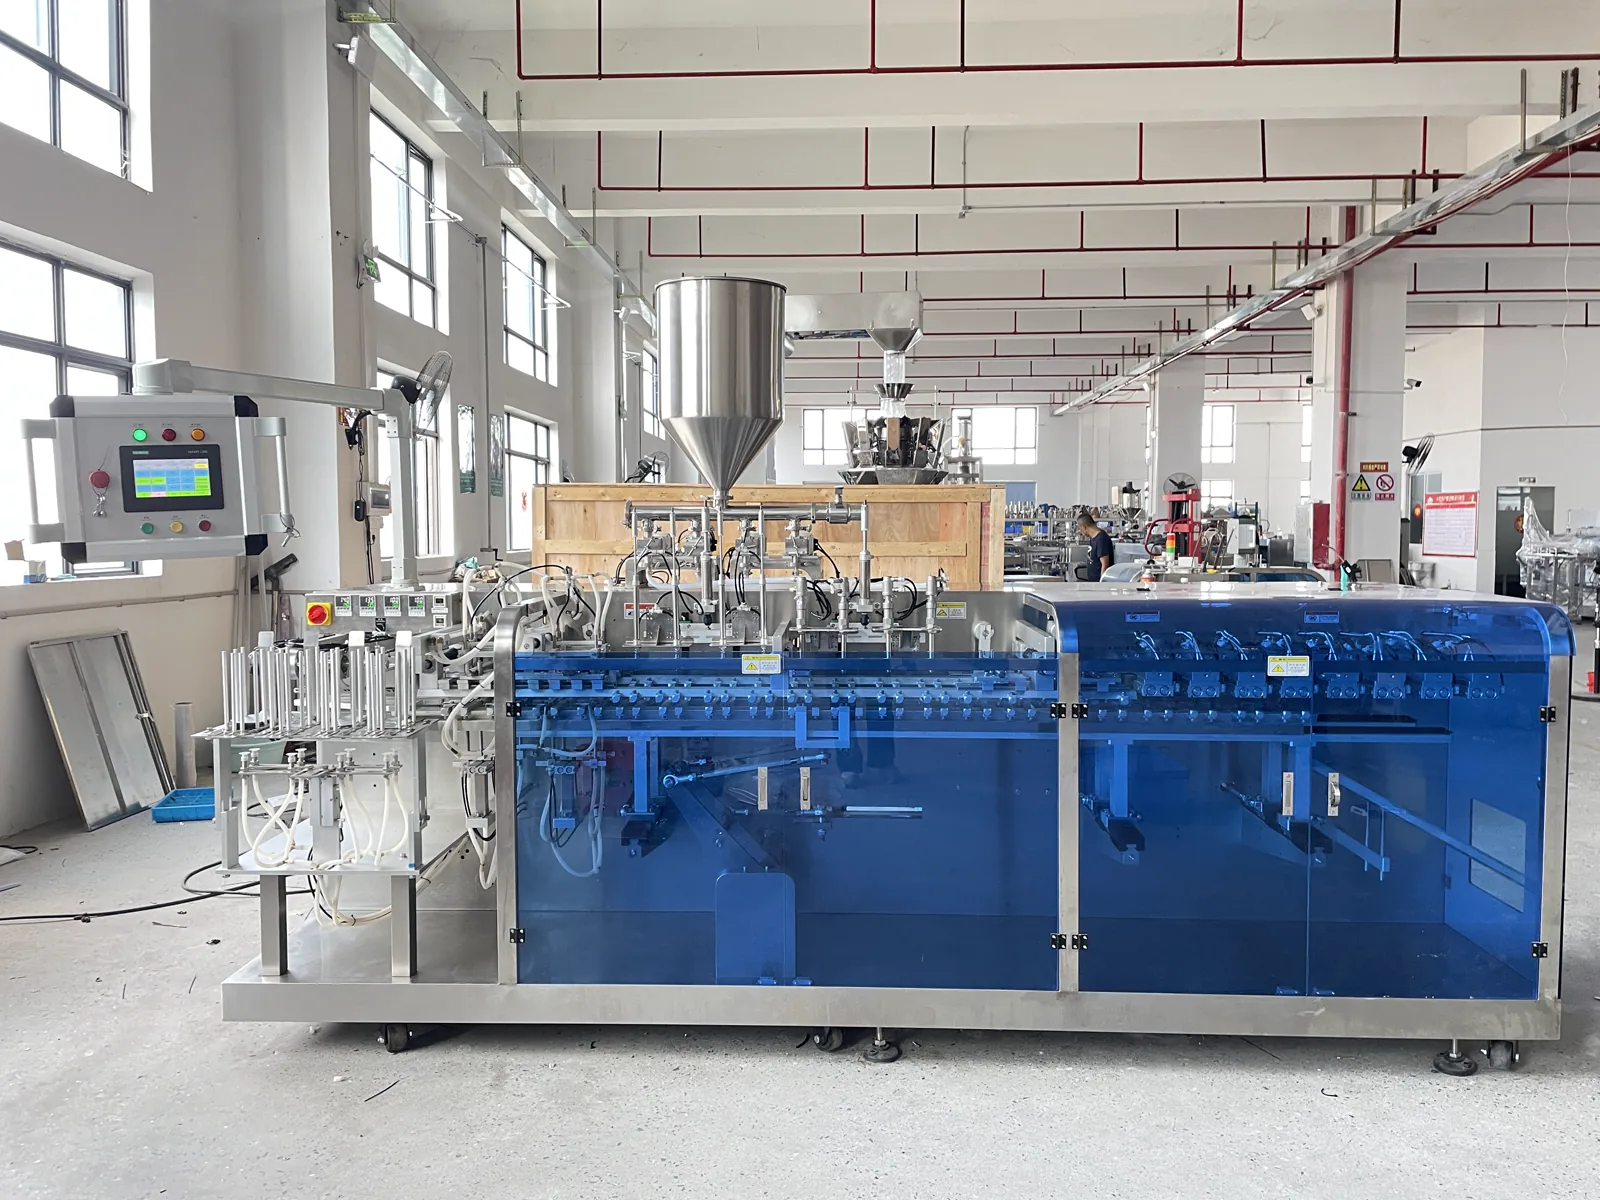
Actual equipment photos from the factory. Confirm the final configuration with the containers, product, sample trials and agreed equipment scope.
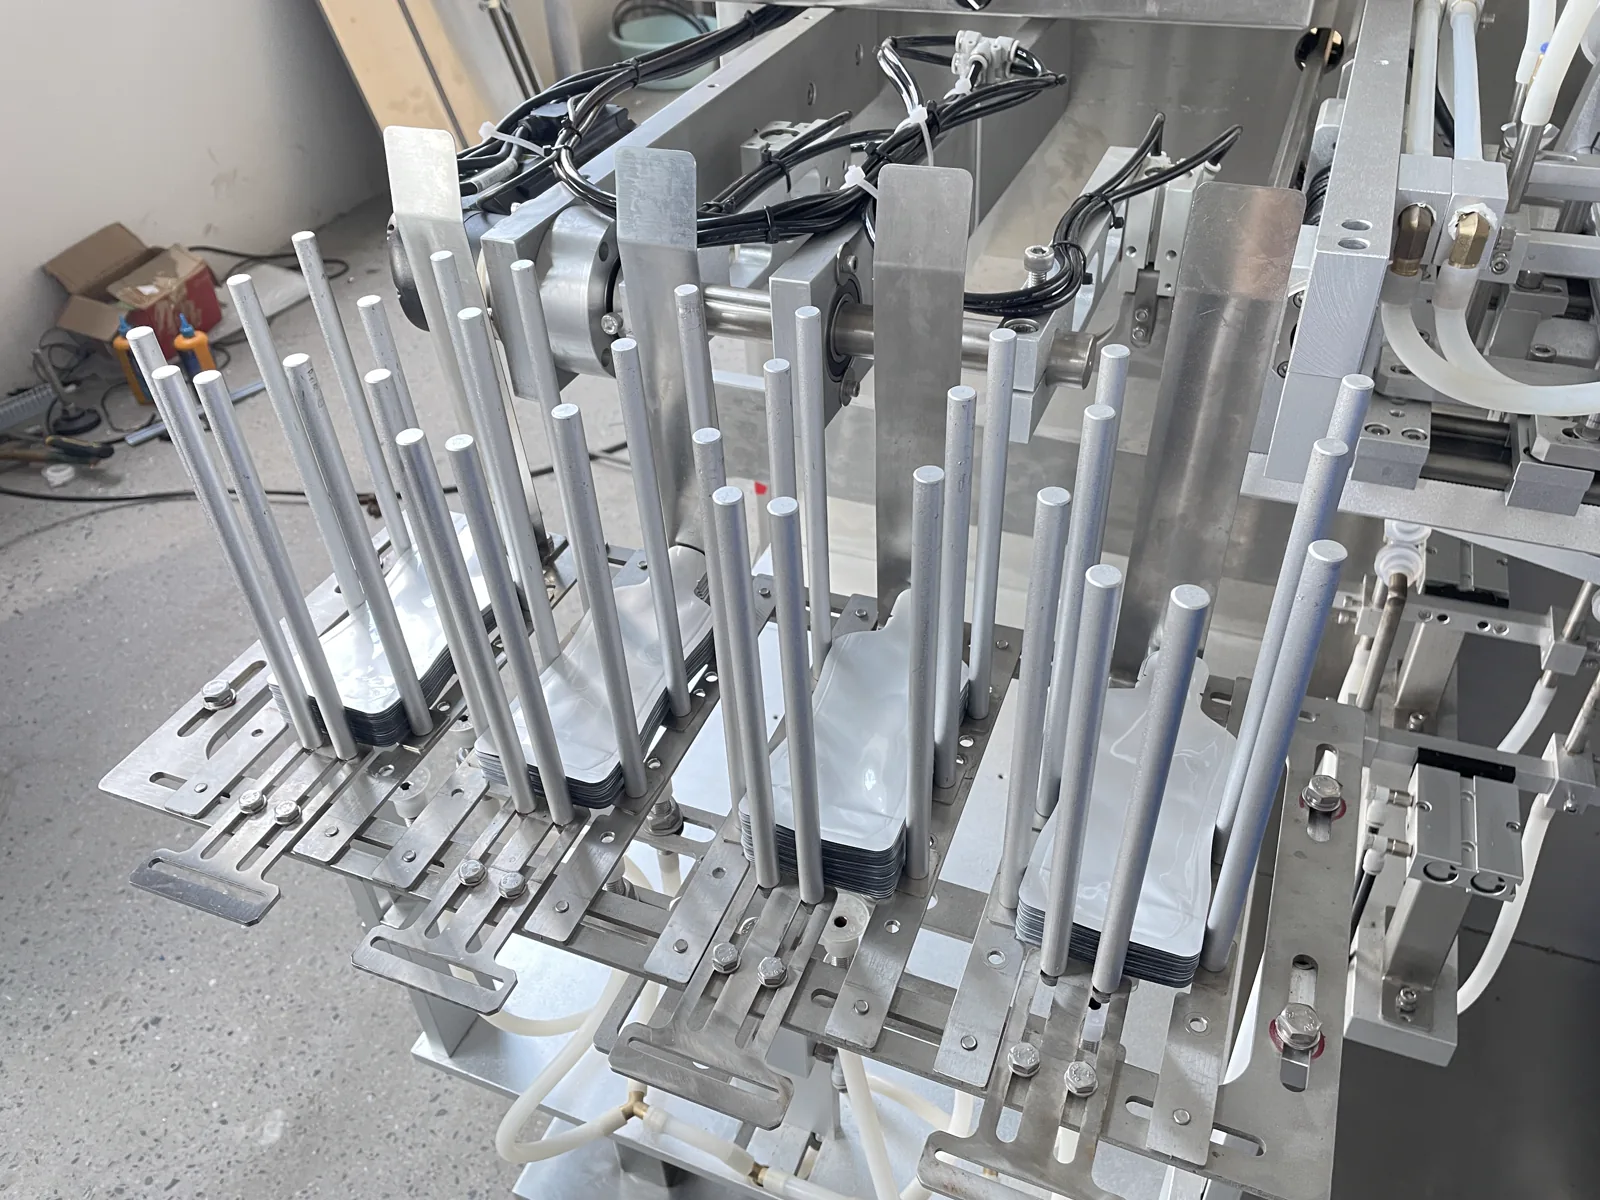
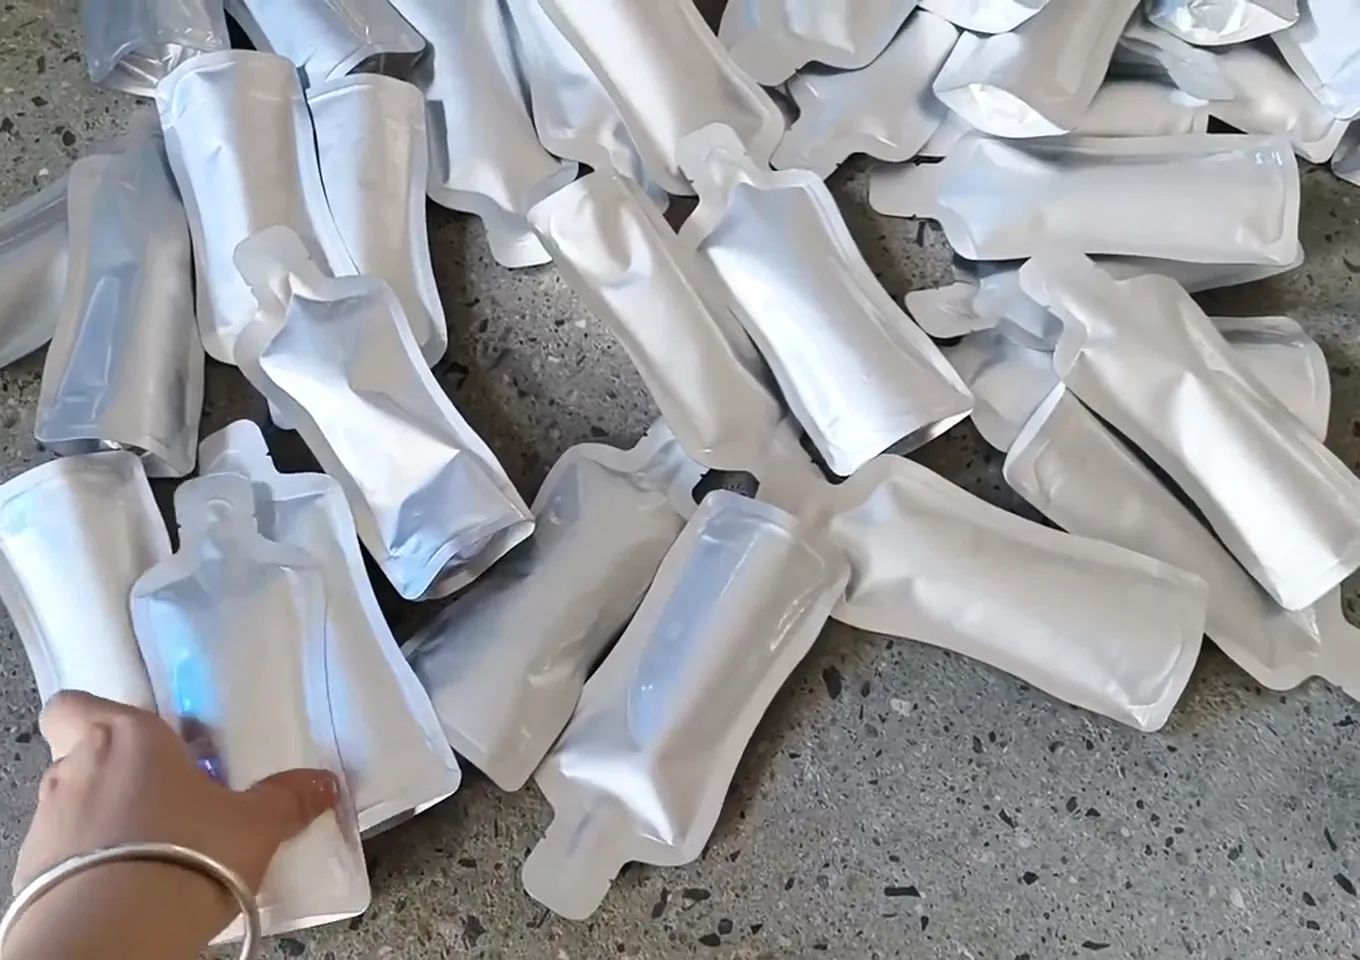
First see real working conditions
Please provide same-batch empty bags, materials, target weight per bag, continuous feeding method, target cycle time, cleaning requirements, and factory space.
Pre-made bags with uniform specifications, consistent bag mouth, and continuous bag supply; special zipper bags or irregular bags require separate trials
Heat-sealable pre-made bags of consistent batch; bag thickness, friction, static, opening, and heat-seal layer must be verified; four-lane bag feeding and picking, bag opening, optional multi-lane metering filling, bag mouth finishing, multi-lane heat sealing, and merging discharge
Optional multi-lane metering, bag opening detection, filling confirmation, no-fill-no-seal, rejection, merging conveying, and data interface.
Please provide same-batch empty bags, materials, target weight per bag, continuous feeding method, target cycle time, cleaning requirements, and factory space.
First see real working conditions
The more complete the samples, packaging materials, and site information, the easier it is to determine the equipment route, changeover scope, and line integration boundaries.
First see real working conditions
Confirmed based on four-lane bag supply consistency, metering distribution, bag opening success rate, bag mouth cleanliness, and sealing pressure holding. Actual capacity is confirmed by project trials.
Four-lane automatic bag feeding and sealing; multi-lane metering, inspection, rejection, merging conveying are optional per project
Pre-made bags with uniform specifications, consistent bag mouth, and continuous bag supply; special zipper bags or irregular bags require separate trials
Liquids, powders, granules, or small products with flowability and feeding stability suitable for multi-lane distribution
Heat-sealable pre-made bags of consistent batch; bag thickness, friction, static, opening, and heat-seal layer must be verified
Four-lane bag feeding and picking, bag opening, optional multi-lane metering filling, bag mouth finishing, multi-lane heat sealing, and merging discharge
Evaluate synchronous adjustment of four sets of bag magazines, suction cups, grippers, discharge openings, sealing guides, and programs based on bag type
Confirm equipment dimensions, power supply, air supply, maintenance space, and upstream/downstream interfaces based on multi-lane drives, metering distribution, sealing area, merging conveying, and maintenance access
Use same-batch bag samples to check bag feeding, picking, opening, and heat sealing performance.
Determine multi-lane metering, buffering, discharge sequence, and anti-cross-contamination measures.
Check synchronous actions, abnormal lanes, bag magazine replenishment, and finished product merging.
Accept according to agreed operating duration, pass criteria, cleaning, and changeover requirements.
Common configuration routes
Single-lane systems simplify changeovers and exception handling; four lanes suit stable pouch and product projects. Lane count never replaces a complete pouch-and-material trial.
Suitable for projects with more specifications or moderate output targets; changeover and maintenance are relatively centralized.
Suitable for projects with stable bag types, continuous material supply, and matching multi-lane metering.
Configure some lanes first or reserve interfaces; subsequent expansion must confirm structural and control boundaries in advance.
Four-lane parallel pouch packaging
First see real working conditions
It is generally more suitable for batch projects with stable specifications. Frequent changeovers involve synchronous adjustment of multiple bag magazines, grippers, discharge, and sealing positions; changeover time and scope should be calculated first.
Depends on control, feeding, and merging design. If lane isolation or degraded operation is required, the exception handling logic must be clarified during the proposal stage.
Send samples and requirements
Send complete premade pouches, mouth and seal-layer details, product samples, dose and tolerance, dust and venting behaviour, target cycle, cleaning/changeover needs and upstream/downstream interfaces.