Check applicable objects first
Regular single pieces, grouped products or tray-loaded products that can be continuously conveyed; dimensions and orientation confirmed by actual sample
Three-servo flow wrapping
The machine horizontally flow-wraps regular single or grouped products. Confirm dimensions, rigidity and surface, orientation and spacing, film width, thickness and sealant, longitudinal/end-seal positions, cutting, coding and line interfaces through continuous trials with the actual product and rollstock.
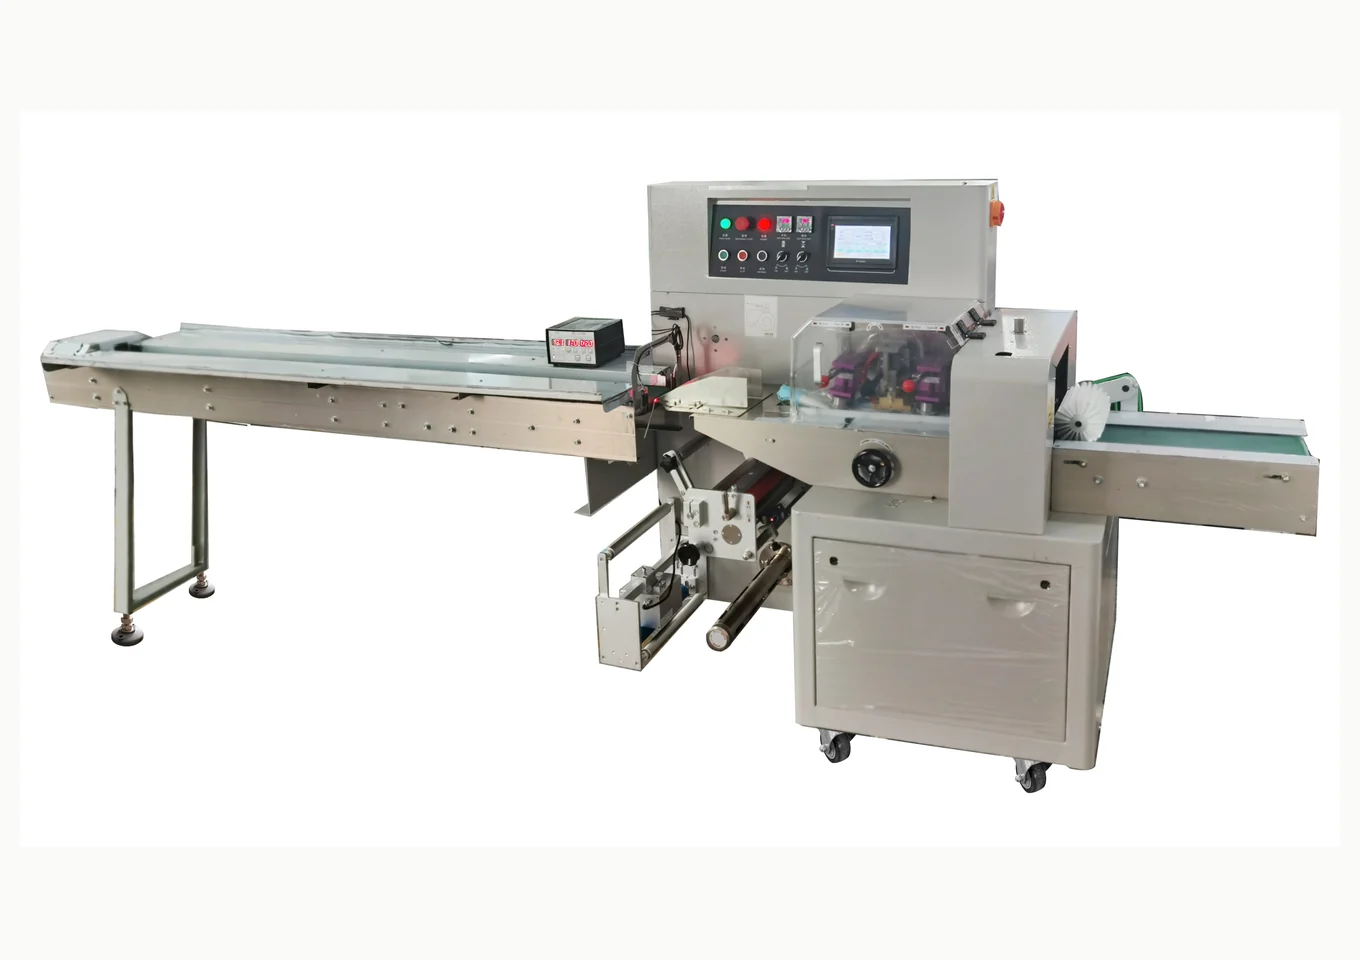
Actual equipment photos from the factory. Confirm the final configuration with the containers, product, sample trials and agreed equipment scope.


See actual working conditions first
Please provide actual product, dimensions and weight range, feeding orientation, roll film samples, seal appearance, target speed and upstream interface.
Regular single pieces, grouped products or tray-loaded products that can be continuously conveyed; dimensions and orientation confirmed by actual sample
Heat-sealable roll film; film width, thickness, friction, print registration and heat seal layer confirmed by sample; product infeed, roll film unwinding, bag forming, longitudinal sealing, end sealing and cutting, finished product output
Optional automatic feeding, coding, gas flushing, punching, tear notch, metal detector interface, rejection and finished product conveyor.
Please provide actual product, dimensions and weight range, feeding orientation, roll film samples, seal appearance, target speed and upstream interface.
See actual working conditions first
The more complete the samples, packaging materials and site information, the easier it is to determine the equipment route, changeover scope and line integration boundaries.
See actual working conditions first
Confirmed based on product length, infeed pitch, film running, sealing time and upstream feeding stability. Actual capacity is confirmed by project trials.
Three servos coordinate infeed, film feeding and end sealing; coding, gas flushing, punching, inspection and automatic feeding are optional per project
Regular single pieces, grouped products or tray-loaded products that can be continuously conveyed; dimensions and orientation confirmed by actual sample
Solid food, daily necessities, industrial small parts or tray-loaded products; surface condition, fragility, stickiness and feeding orientation must be specified
Heat-sealable roll film; film width, thickness, friction, print registration and heat seal layer confirmed by sample
Product infeed, roll film unwinding, bag forming, longitudinal sealing, end sealing and cutting, finished product output
Adjust or replace bag former, film guides, conveyor, longitudinal seal and end seal positions according to product dimensions and film width
Confirm equipment dimensions, power, air supply, maintenance space and upstream/downstream interfaces based on servo axes, heat sealing, conveyor length, film stand and optional feeding or inspection modules
Confirm dimension range, feeding orientation, film width, heat seal layer and friction performance.
Select bag former, longitudinal seal, end seal, cutting and printed film registration solution.
Verify product pitch, film feeding, end seal position and abnormal stop logic.
Accept according to agreed product, film material, speed, sealing and changeover requirements.
Common configuration routes
Standard flow wrapping forms and seals a pack. A shrink route additionally needs product heat tolerance, shrink film, venting, tunnel conditions and cooling; it is not a temperature-only add-on.
Manual or existing conveyor infeed, completes bag forming, longitudinal sealing, end sealing and cutting.
Product is first placed into a tray, then wrapped by the flow wrapper main unit; tray stability must be verified.
Can add coding, gas flushing, punching, inspection or automatic feeding, with interfaces confirmed separately.
Three-servo flow wrapping
See actual working conditions first
No. It is only a series identifier; the actual usable film width, product dimensions, speed and structure must be based on the final configuration and sample testing.
It can be evaluated, but the adjustment range of the bag former, conveyor, end seal position and program is limited; a complete dimension list is required to confirm whether parts need to be changed.
Send samples and requirements
Send product samples or dimensions and weight, rigidity and surface, orientation and spacing, film structure and width, seal and cut positions, coding, target cycle and line interfaces.