Model / Identity
YJ-IF610
Custom machine | Sample-confirmed
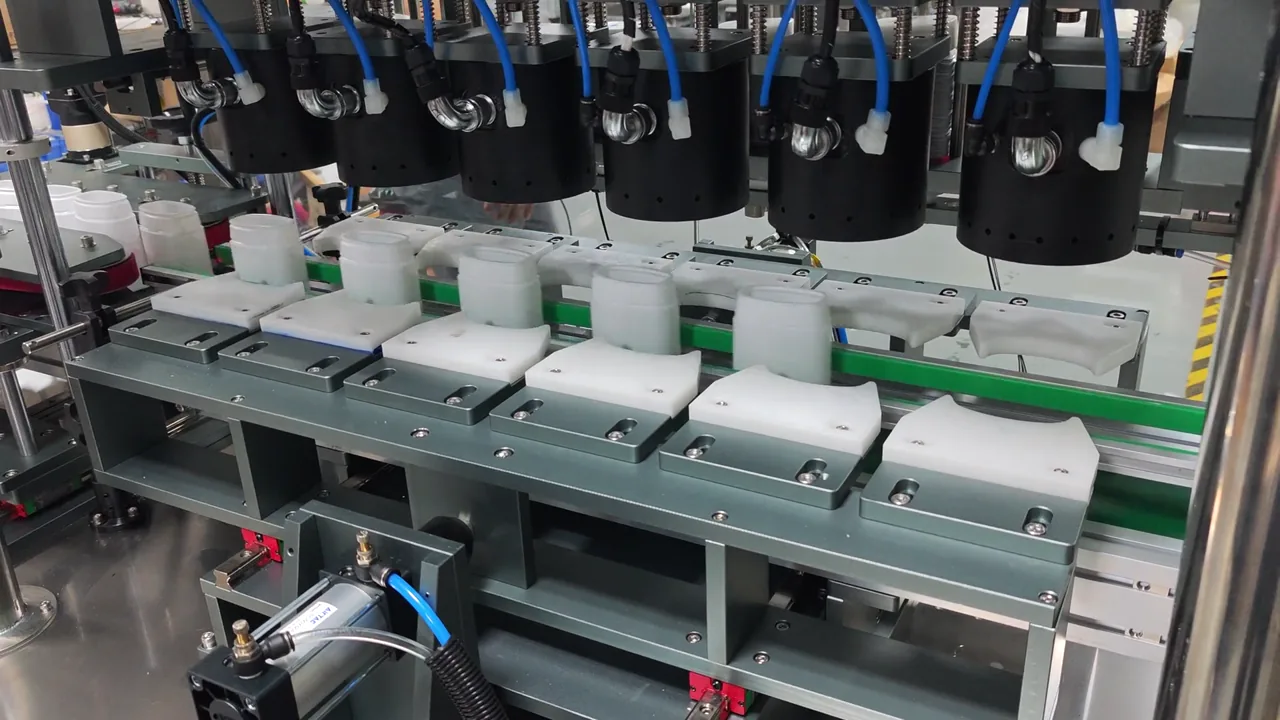
For inline induction foil sealing at the bottle mouth before an outer cap is fitted. First-party media verifies the current six-head machine, conveyor, locating carriers and enclosed frame; the series can be engineered with 1–8 sealing heads. Head count is selected from container pitch and mouth size, foil assembly, per-container process time, changeover and adjacent-line cycle, then confirmed with real sample trials.
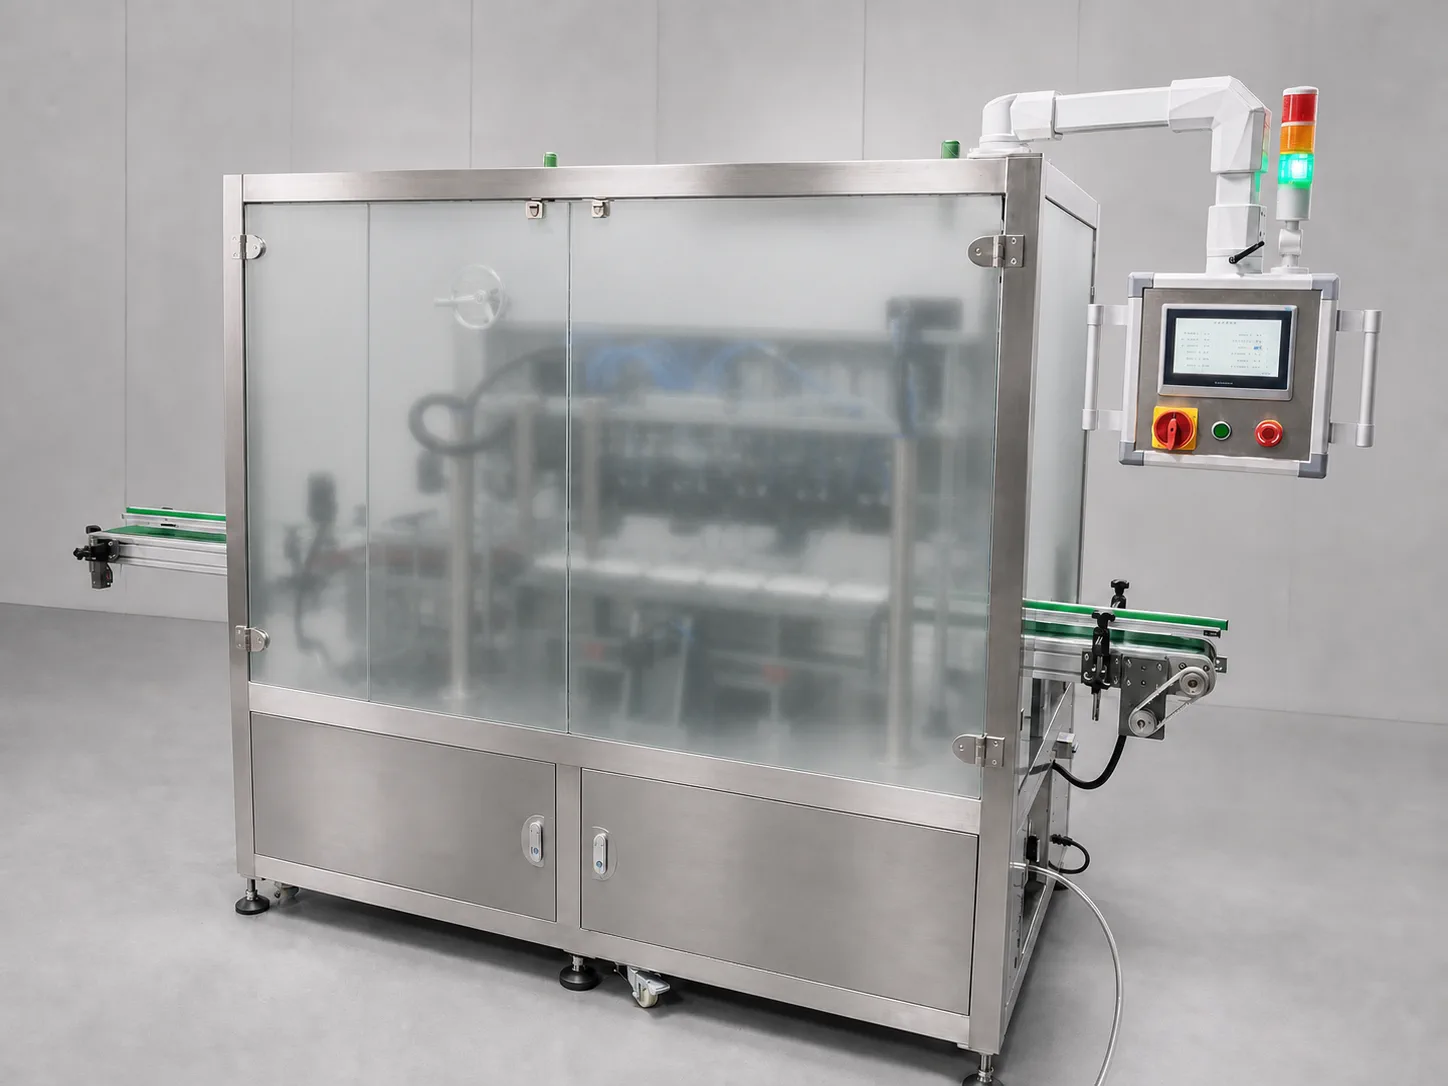
View operating media
First-party video of the current six-head machine showing inline conveying, locating carriers and six sealing heads. The series is configurable with 1–8 heads; video duration is not an output claim.
Evidence boundary
Content follows the available evidence and visible structure. Unverified figures are not presented as commitments.
YJ-IF610
Independent custom line; configuration is confirmed from samples and project requirements.
No preset range; verify with real samples, per-container process time, the selected 1–8 head configuration and the complete line cycle.
Configurable 1–8 head inline custom line; current media shows a six-head machine. Infeed, positioning, release and controls are project-confirmed.
Evidence boundary
Provide containers, foil assemblies, per-container process time, target cycle, adjacent machines, conveyor height and layout. Trial sealing is used to select the exact 1–8 head configuration, carriers, interlocks and acceptance method.
Evidence boundary
Content follows the available evidence and visible structure. Unverified figures are not presented as commitments.
YJ-IF610
Independent custom line; configuration is confirmed from samples and project requirements.
No preset range; verify with real samples, per-container process time, the selected 1–8 head configuration and the complete line cycle.
Configurable 1–8 head inline custom line; current media shows a six-head machine. Infeed, positioning, release and controls are project-confirmed.
Containers receiving induction foil sealing before an outer cap is fitted; material and mouth structure to be confirmed.
To be confirmed from samples, mouth dimensions, body size, height and line spacing.
Bottled products; contents and their effect on the induction process require review.
Induction foil liner assembly; laminate structure, thickness and container compatibility to be confirmed.
Configuration choice
Provide containers, foil assemblies, per-container process time, target cycle, adjacent machines, conveyor height and layout. Trial sealing is used to select the exact 1–8 head configuration, carriers, interlocks and acceptance method.
Provide physical samples, dimensions and target requirements.
Confirm the process, locating, changeover and integration boundary.
Use representative samples to verify the result and complete cycle.
Approve the technical agreement, supply scope and quotation.
Configuration choice
The current six-head media verifies the structure; it does not mean every project needs six heads. More heads improve usable output only when pitch, positioning, induction time and adjacent-line supply remain synchronized.
Custom machine | Sample-confirmed
The current six-head media verifies the structure; it does not mean every project needs six heads. More heads improve usable output only when pitch, positioning, induction time and adjacent-line supply remain synchronized.
Evidence boundary
Content follows the available evidence and visible structure. Unverified figures are not presented as commitments.
It is engineered with 1–8 sealing heads, locating carriers and an enclosed inline frame for projects requiring multiple stations, controlled positioning and complete-line integration. Current media shows the six-head machine.
Not necessarily. More heads improve usable output only when container pitch, positioning, foil process time, carrier motion and adjacent-line supply remain synchronized. Test the complete cycle for the selected 1–8 head configuration.
The inline conveyor is visible, but conveyor height, speed, interfaces, interlocks, infeed and discharge must be confirmed from the site layout.
Send containers, foil components, output target, adjacent equipment, layout, power standard and acceptance criteria.
Send line details
Do not send target hourly output alone. Container samples, foil assembly, process time, pitch and adjacent-line cycle are required to decide whether one, six or another head count is appropriate.