Solution topic
Rotary Multi-Station Cup and Tray Line: Filling and Sealing, Vacuum Tray, and Pre-Cut Film Pick-and-Place
Compare rotary small-cup filling and sealing, precut-film sealing for boxed facial masks, and vacuum tray sealing. Review containers, products, films, stations, coding, checkweighing and sample trials before purchase.
Project Setup & Equipment Selection
These are route and equipment options, not a list of items included as standard or connected in sequence. Confirm the final configuration against samples, process requirements and site interfaces.
| Process | Equipment or Supporting Information | Configuration Notes |
|---|---|---|
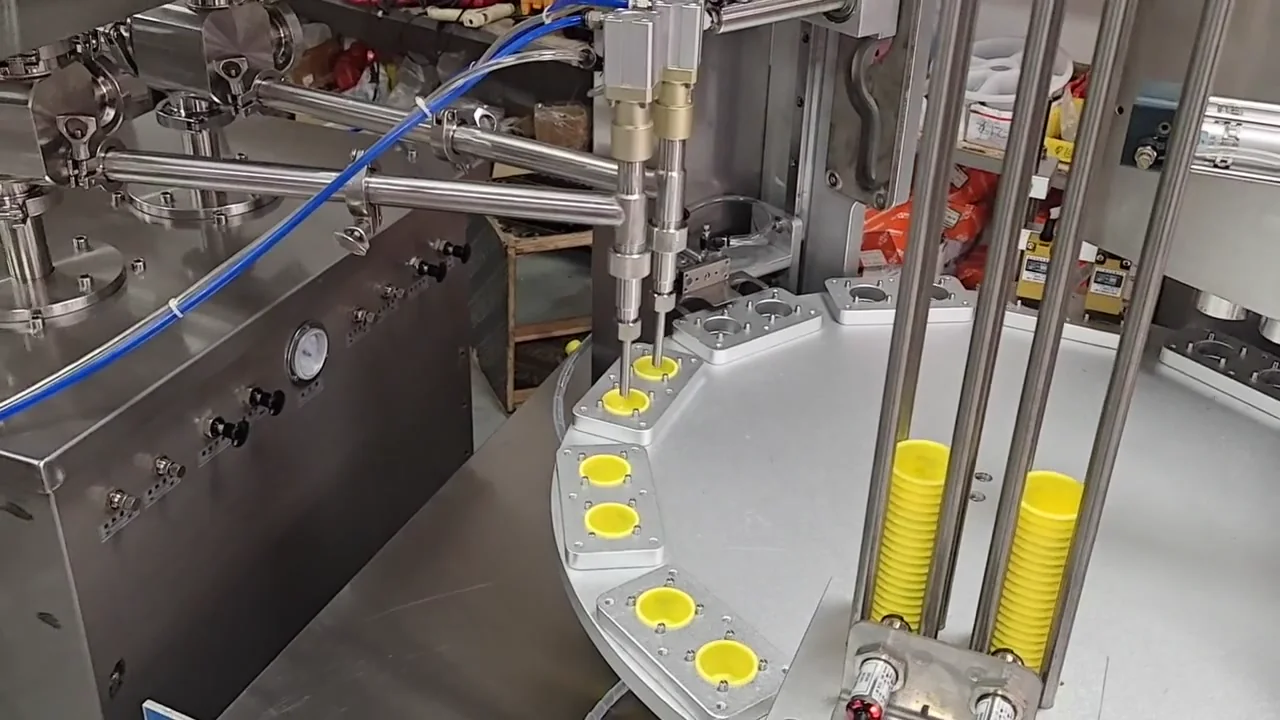
| Rotary Small-Cup Filling and Sealing Machine | Rotary Small-Cup Filling and Sealing Machine | Position, fill and heat-seal lidding film on small cups using rotary stations. The real machine footage shows a two-up configuration. Cup design, product, lidding material and target output are confirmed with samples. |
| Vacuum tray branch | Rotary Turntable Vacuum Tray Sealing Machine | Used separately when the tray project explicitly requires vacuum sealing; the packaging structure and vacuum target cannot be replaced by regular heat sealing conditions. |
| Sheet film supply and sealing | Automatic Pre-Cut Lid Pick-and-Place Tray Sealer | For the pre-cut lid film route, complete separation, pick-and-place, and sealing; sheet stacking state and tray references need joint testing. |
| Batch and Weight Inspection | Date & Batch Inkjet Printer Inline Checkweigher | After sealing is completed, add variable information and weight verification; the trigger position, judgment values, and exception handling are written into the acceptance items. |
| Rotary Filling and Sealing Machine for Facial Mask Boxes | Rotary Filling and Sealing Machine for Facial Mask Boxes | When filling and sealing boxed sheet-mask products, the box position, product dose and lidding film need to work together. A rotary machine can arrange these steps across stations; two-up and four-up versions use different tooling. Test your box, product and film samples to determine the suitable number of positions, fill volume and sealing method. Compare complete main machines as alternatives for the same packaging task; they are not a default sequence of two filling and sealing machines. |
- The value of the rotary table structure lies in assigning cup feeding, filling, film placement, sealing, and discharge to fixed stations, but since cup and tray shapes, contents, and sealing targets differ, the main machine solutions cannot be interchanged.
Solution summary prepared for you
- The conclusion is that the rotary solution is suitable for consolidating cup/tray positioning, filling, film placement, sealing, and discharge into fixed stations, but cup/tray filling and sealing, vacuum trays, and sheet film pick-and-place must be selected as separate branches.
- Compare rotary small-cup filling and sealing, precut-film sealing for boxed facial masks, and vacuum tray sealing. Review containers, products, films, stations, coding, checkweighing and sample trials before purchase.
- Only after providing cups/trays, contents, film, station actions, target cycle time, and discharge direction can the mold, rotary cycle time, and inkjet coding/checkweighing interfaces be determined.
Route comparison
- For small-cup projects with the cup, fill volume and product defined, combining cup loading, dosing, lid placement, heat sealing and discharge on rotary stations. For boxed facial masks, compare the separate box-machine route below.
- Position, fill and heat-seal lidding film on small cups using rotary stations. The real machine footage shows a two-up configuration. Cup design, product, lidding material and target output are confirmed with samples.
- The number of stations, molds, and cycle time must be measured with actual cups, trays, and materials; if the specification range is too wide, changeover and cleaning become more complex.
- When containers, fill volumes, or materials change frequently and only independent sealing is required, it is not advisable to lock in a complete rotary filling and sealing main machine first.
- Rotary Small-Cup Filling and Sealing Machine
- Suitable for projects where tray packaging has clearly proposed a vacuum sealing target and the packaging structure needs independent verification.
- The rotary vacuum tray sealing machine organizes tray positioning and sealing for the vacuum process and does not replace it with ordinary heat sealing conditions.
- Tray rigidity, film, and vacuum targets must be confirmed as a set; results from ordinary cup and tray filling/sealing cannot be directly extrapolated.
- When the project only requires ordinary edge sealing or the vacuum target is not yet defined, the vacuum branch should not be added.
- Use the rotary vacuum tray sealing machine to test trays separately and clearly write out the packaging and acceptance conditions.
- Suitable for projects where film dimensions, stacking, and tray reference are already fixed and automatic sheet separation, sealing, and batch verification are required.
- The automatic pre-cut film pick-and-place tray sealing machine handles film sheet separation and positioning; after sealing, it can be connected to date coding and online checkweighing.
- Film static, orientation, tray opening coverage, and checkweighing judgment all require separate testing and cannot be treated as a fixed downstream section for all rotary projects.
- When film and tray specifications are not yet frozen, or there are no traceability and weight rules, it is not advisable to add the complete downstream section at once.
- Design an independent branch line or interface in the order of film pick-and-place sealing, date and batch coding, and online checkweighing.
- Projects that need metered filling in pre-made boxes and closure with pre-cut sealing film.
- The reference main machine can provide dual-channel metering, pre-cut film pick-and-place, simultaneous two-cavity heat sealing, and mechanical box discharge.
- Manual box placement method, box format, product, film, and trial-run rate must each be confirmed.
- The finished product needs automatic folding, counting, and placement of facial mask sheet material, but that operation is not configured in the solution.
- Use the rotary filling and sealing machine for boxed facial masks as the main machine; evaluate downstream equipment separately by interface.
Associated Equipment / Consumables
Rotary Small-Cup Filling and Sealing MachinePosition, fill and heat-seal lidding film on small cups using rotary stations. The real machine footage shows a two-up configuration. Cup design, product, lidding material and target output are confirmed with samples.
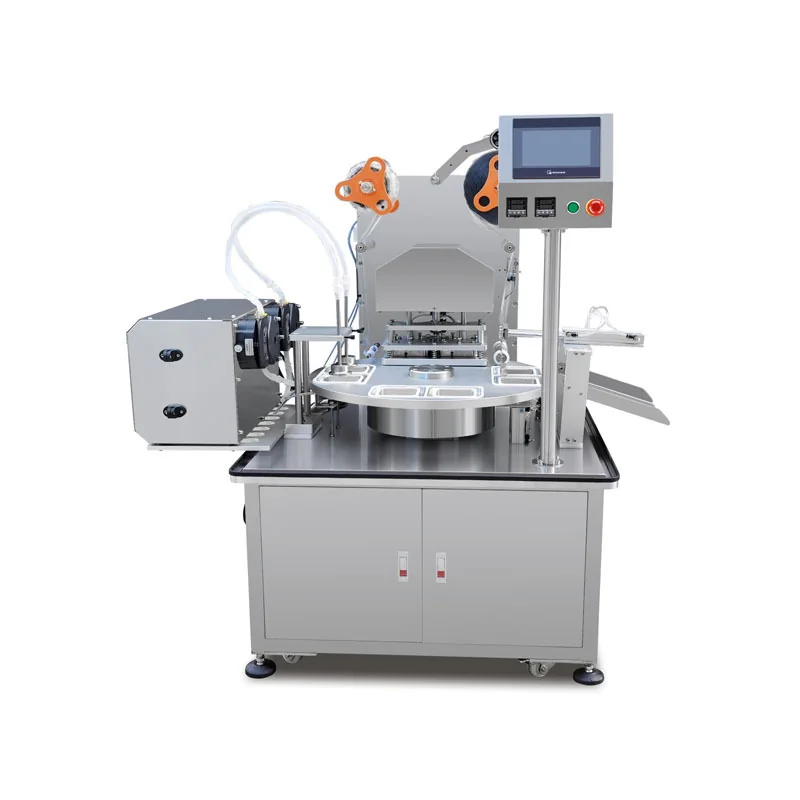 Rotary Turntable Vacuum Tray Sealing Machine
When the vacuum target is clear, use a rotary vacuum tray sealing machine. The sheet film route is handled by automatic pick-and-place equipment.
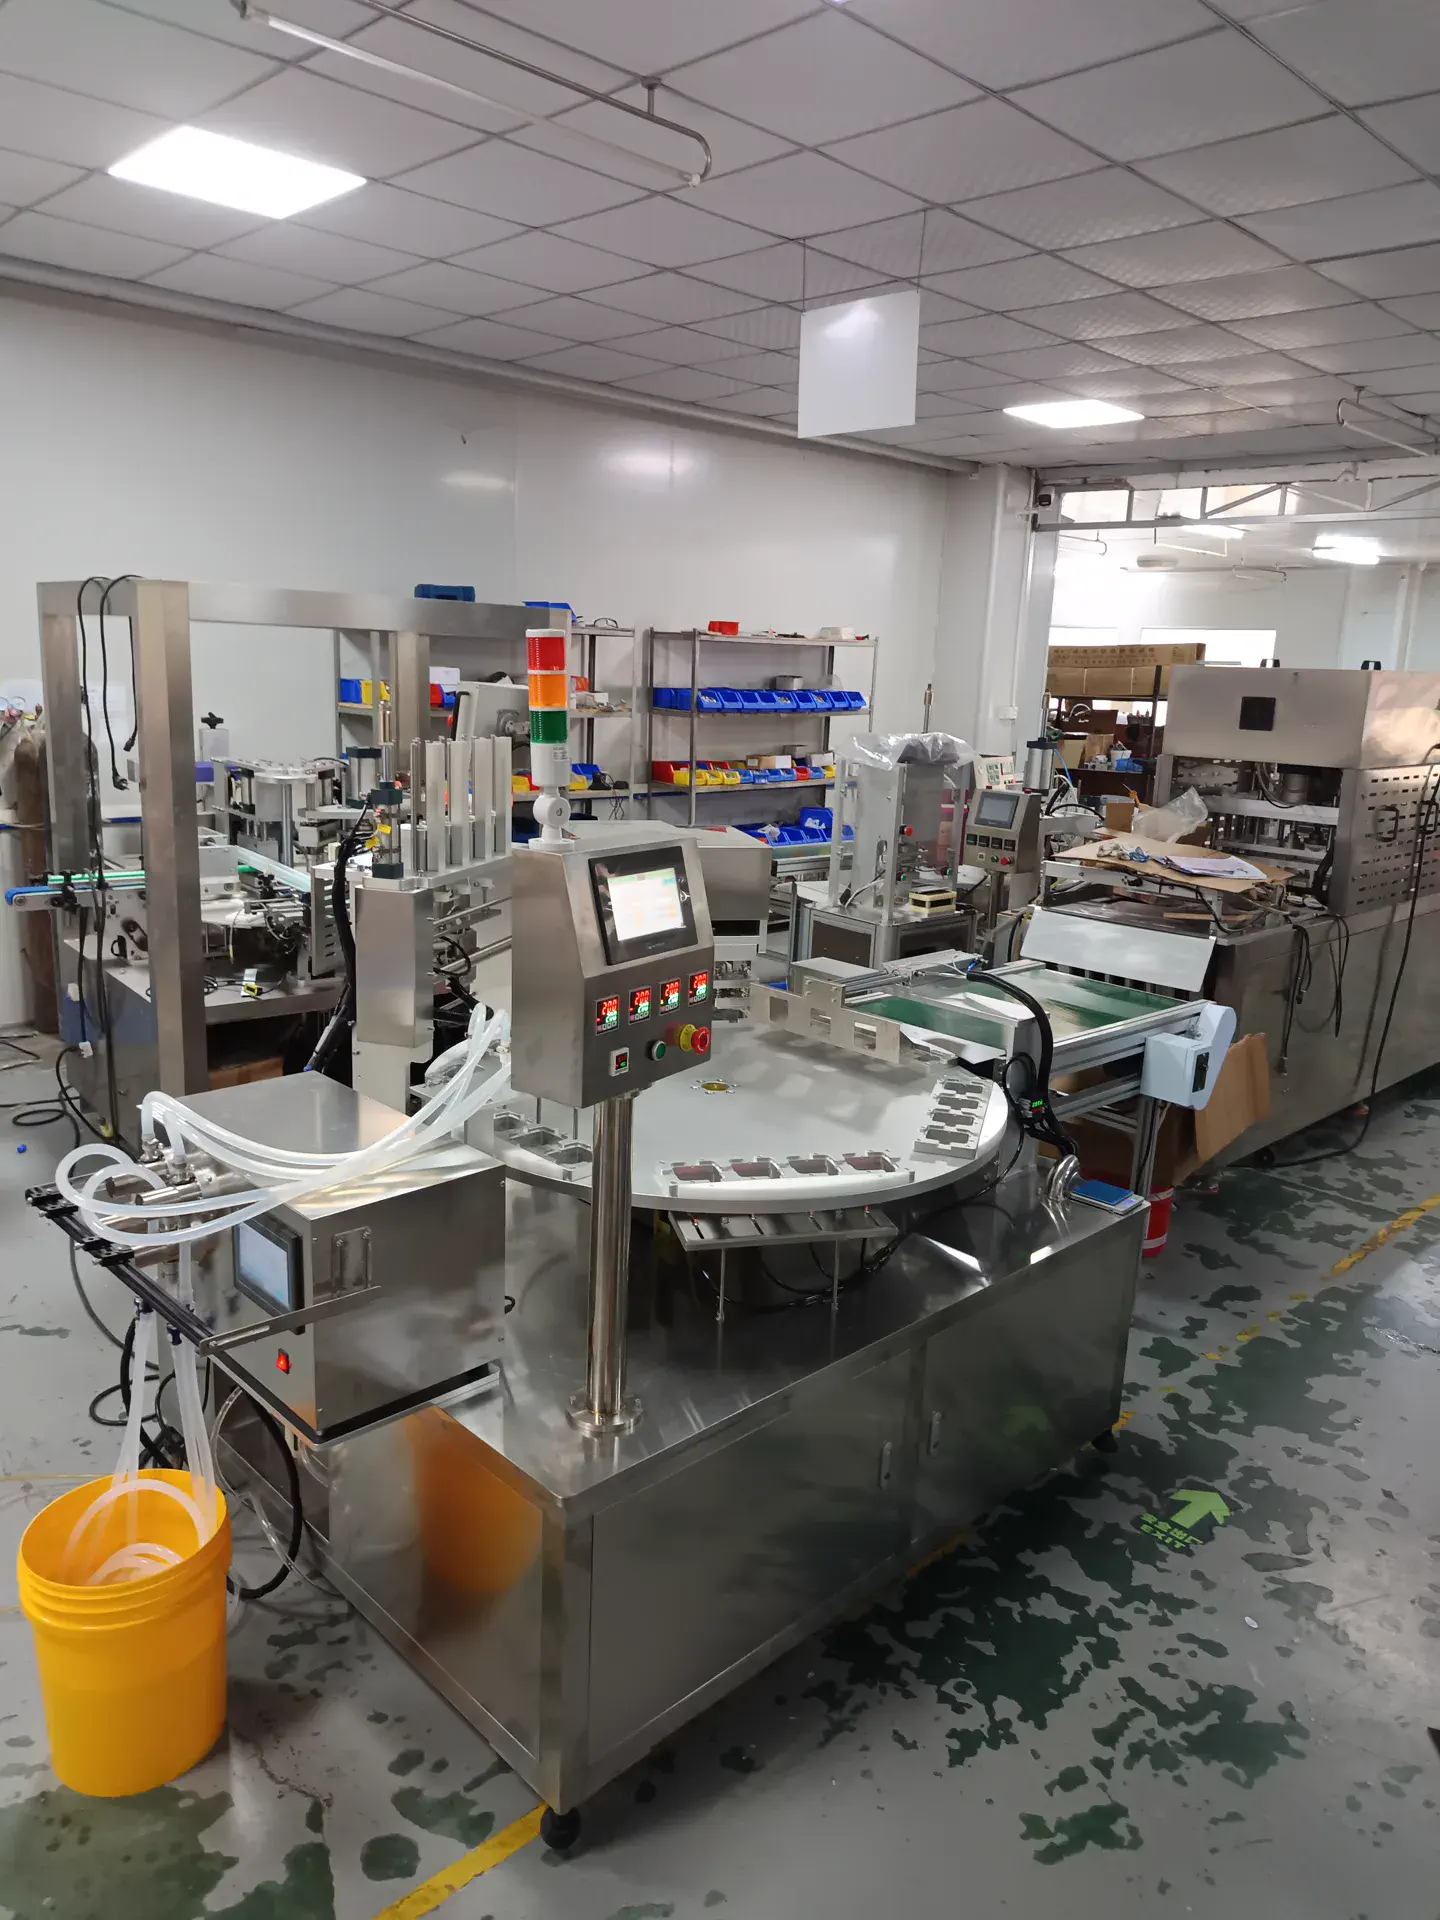 Rotary Filling and Sealing Machine for Facial Mask Boxes
Use production boxes and actual product to confirm positioning, metering and operator cycle.
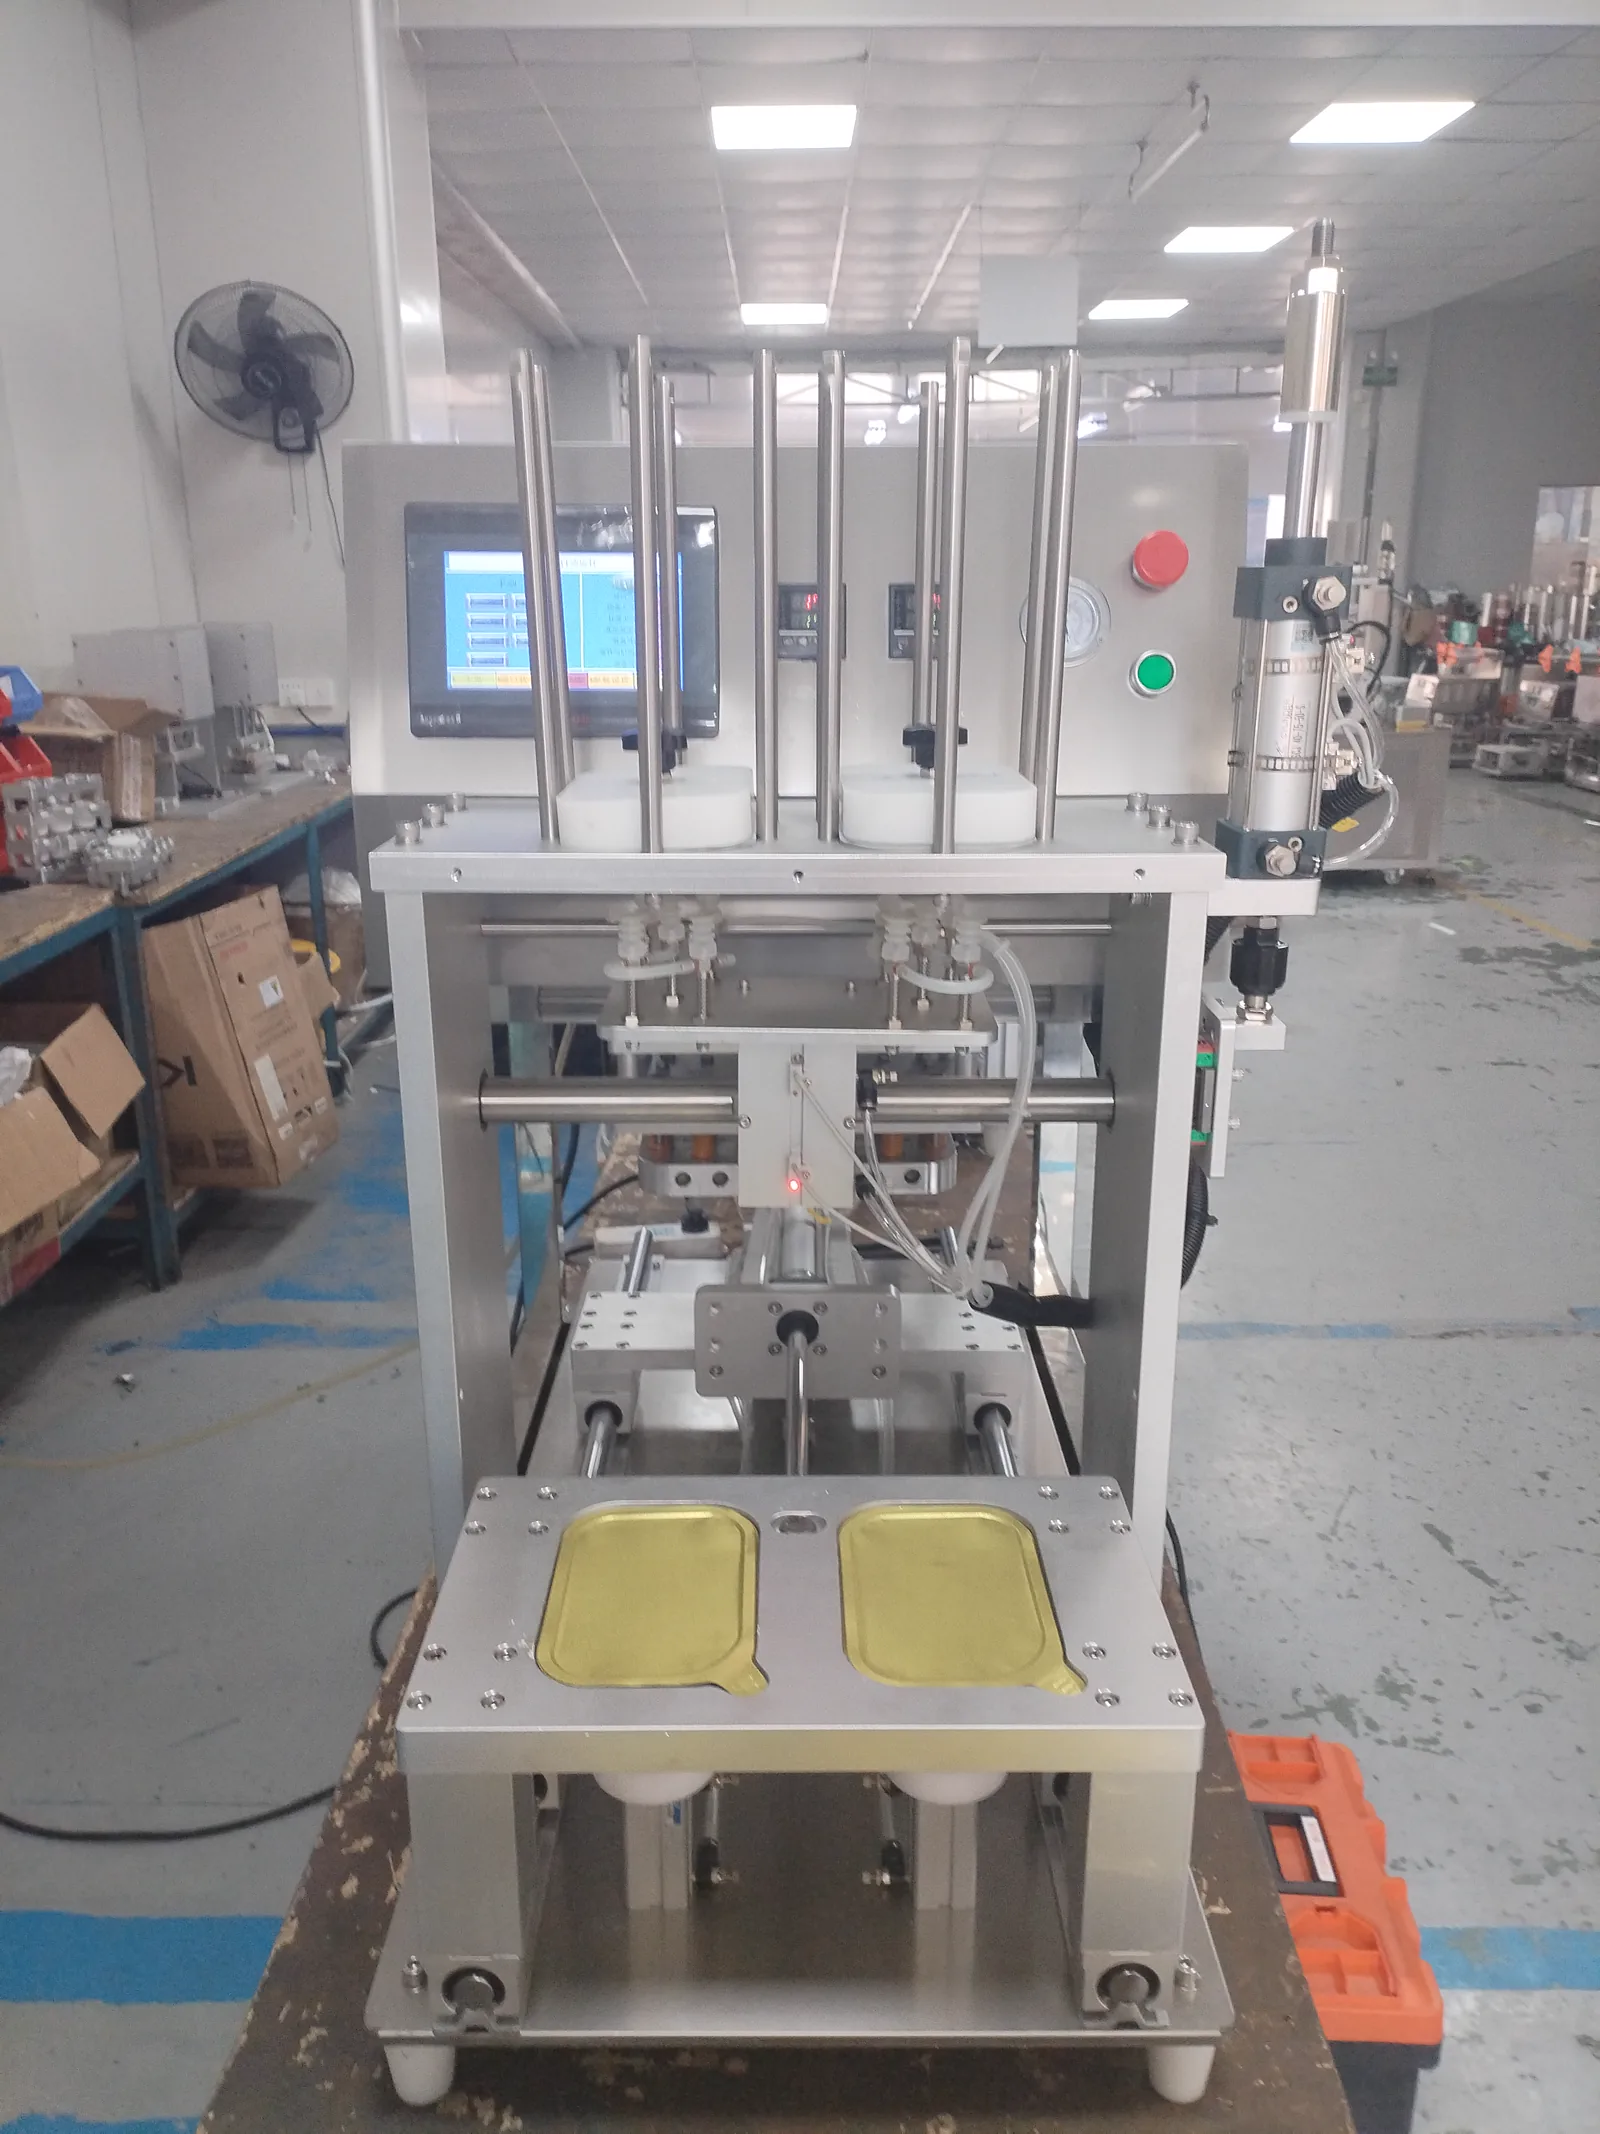 Automatic Pre-Cut Lid Pick-and-Place Tray Sealer
When the vacuum target is clear, use a rotary vacuum tray sealing machine. The sheet film route is handled by automatic pick-and-place equipment.
Core process
First confirm filling, sealing edge cleanliness, and pick-and-place conditions with cups/trays, contents, and film, then arrange the rotary stations.
Position, fill and heat-seal lidding film on small cups using rotary stations. The real machine footage shows a two-up configuration. Cup design, product, lidding material and target output are confirmed with samples.
Tray shape, depth, and film supply method determine the mold, positioning, and film pick-up structure.
When the vacuum target is clear, use a rotary vacuum tray sealing machine. The sheet film route is handled by automatic pick-and-place equipment.
After sealing, add batch information and weight judgment; the trigger position is determined by the discharge orientation.
Prepare molds, seals, and cleaning consumables for common cup/tray specifications, and reserve necessary upstream and downstream interfaces.
Use production boxes and actual product to confirm positioning, metering and operator cycle.
Sample details
Specify whether it is cup/tray filling and film sealing, vacuum tray, or pre-cut sheet film tray, and provide the finished product form to separate the three equipment branches.
Actual cup/tray samples, finished product photos, sealing goals, and current project stageShape, depth, rim, and stacking affect the rotary tooling; the film form determines whether roll film, sheet film, or vacuum sealing structure is used.
Key dimensions, rim, stacking state, roll film or sheet film samples, and orientationMaterial flow, particles, target fill volume, and sealing edge contamination risk change the feeding and filling stations; use samples representative of production state.
Actual contents, fill volume, material state, cleaning requirements, and sealing edge cleanliness standardsConfirm cup feeding, filling, film placement, sealing, vacuum, discharge, inkjet coding, and checkweighing item by item, and clarify which belong to the main machine and which are independent branches.
Action list, existing equipment, manual involvement, batch marking, and quality verification requirementsCheck the planned cycle time against the full station cycle, and submit on-site direction, power and air supply, changeover frequency, and delivery requirements to define the equipment boundary.
Production cycle time, on-site dimensions, infeed/outfeed direction, power and air supply, changeover plan, and delivery dateCommon selection mistakes
The rotary table is suitable for fixed-station cycles, but vacuum trays, sheet film automation, or complex downstream processes may not need to be forced into the same platform.
Container shape, stacking, rim, and discharge orientation change the tooling and actions. Without actual samples, the station plan is prone to rework.
Cup feeding, positioning, film placement, sealing, cooling, and discharge together form the cycle; any station can become a bottleneck.
Vacuum trays have a separate packaging structure and target; regular cup/tray heat sealing cannot perform the same process.
Instability in dimensions, static, stacking, and orientation affects separation and positioning; the sheet film must be frozen before automation.
View detailed technical notes
Choose the container and process before the rotary stations
Rotary describes the machine layout, not the sealing process. Cups, trays, bottles and jars differ in support, positioning, lid handling and sealing contact surfaces; similar names do not make machines interchangeable. This guide focuses on cups and trays. Bottle and jar projects need a separate check of the neck, film or liner, cap condition and positioning. Establish ordinary heat sealing, vacuum packaging or MAP requirements before combining loading, filling, lid feeding, sealing and discharge.
Ordinary heat sealing, vacuum and MAP require different configurations
Choose the rotary vacuum tray machine only when vacuum packaging is required and the chamber, evacuation and tray resistance have been tested. Ordinary continuous heat sealing is a separate route; a rotary table or conveyor does not automatically provide vacuum or MAP.
Film feeding is an independent technical condition
Pre-cut lid film requires checking dimensions, stacking, static, and orientation. The automatic pre-cut film pick-and-place tray sealing machine can only verify sheet separation, positioning, and sealing after the packaging material is stable.
Two containers per cycle do not mean adding every station time
An indexing table can run separate stations in parallel after positioning. The complete cycle includes indexing, settling, the slowest station and required interlock allowance. Two-up means two containers per cycle, not an unconditional doubling of output. Fill volume, foaming, stringing, lid separation and feeding can limit the cycle. Verify seal quality with agreed product and packaging, then record acceptable output during continuous operation. State changeover, cleaning and replenishment time separately.
Validate filling, lid placement and sealing together
Splashing, drips and liquid movement during indexing can contaminate the rim. Check nozzle position, fill cut-off and headspace together, then establish sealing temperature, pressure and dwell with the actual container and lid. Precut lids require separation, orientation and placement trials. Switching to rollstock also requires a suitable feed and cutting mechanism. Higher heat is not a universal remedy for a distorted rim.
Batch coding and checkweighing are placed after sealing
The date and batch inkjet coder and online checkweigher should be integrated based on a stable discharge orientation. The printing area, judgment values, and exception handling are determined by acceptance rules.
Mold change and cleaning are calculated based on the main specifications
Different cups and trays change the molds, positioning parts, and film; the material also changes the cleaning method. Common specifications, changeover frequency, and spare parts should be itemized in the quotation.
Start with photos, then confirm the complete process
Start with container photos, contents, lid format and approximate output; a complete technical specification is not needed for the first enquiry. Then confirm manual or automatic loading, filling, lid handling, sealing, discharge and changeover. Coding, checkweighing, inspection, rejection and downstream conveying are separate scope items. For an existing line, share conveyor height, direction, buffering and start-stop requirements.
Reserve process boundaries when samples are not yet frozen
When cups, trays, film, or vacuum targets are not yet determined, only the equipment direction can be evaluated. The final molds, station combination, and continuous performance must be verified with official samples.
Common questions
What projects are suitable for a rotary multi-station structure?
Position, fill and heat-seal lidding film on small cups using rotary stations. The real machine footage shows a two-up configuration. Cup design, product, lidding material and target output are confirmed with samples.
Can vacuum trays share a machine with regular cup/tray filling and sealing?
They cannot be assumed to be shared. Vacuum trays require a separate packaging structure and vacuum target, so an appropriate machine configuration should be used and validated with tray film materials.
How can pre-cut sheet film be integrated into a rotary project?
First decide whether film separation, pick-and-place and sealing stations belong inside the rotary machine or whether a separate tray sealer is needed. The two are not automatically placed in series. Test separation, orientation, placement and sealing with production film stacks and cup or tray samples, then configure the rotary space, stations and cycle. Roll-film feeding requires a separate structural assessment.
Can inkjet coding and checkweighing be added to the rotary main machine later?
During the layout phase, you can reserve the discharge orientation, trigger position, conveyor length, and signal interface. Whether to add them later should be confirmed based on traceability and quality plans.
Can multiple cup/tray types be produced with just a mold change?
You need to compare differences in shape, depth, rim, pick-and-place, and contents. The main machine may allow mold changes, but positioning parts, film materials, and station actions still need to be tested per specification.
What information should be prepared for exported rotary equipment?
In addition to cup/tray film and materials, you should also provide on-site power and air supply, interface language, technical documentation, spare parts, transport packaging, and remote or on-site service requirements.